+971 55 447 8664 +971 50 514 7060 [email protected]

CE Certified Post Pallet Racks Manufacturers & Direct OEM Engineering

Global Leader in Certified Heavy-Duty Stacking Post Racks, Modular Manurack Storage Systems, and High-Density Industrial Material Handling Solutions

Certified Heavy-Duty Warehouse Storage Solutions

Explore our precision-engineered, CE-compliant pallet racking, stacking post frame modules, wire mesh decking, and industrial safety infrastructure.
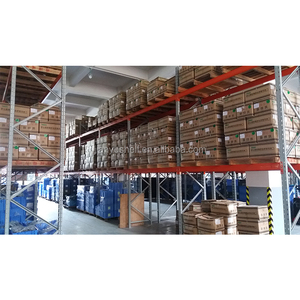
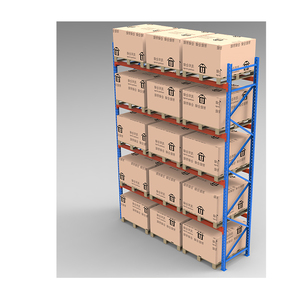
Commercial Industrial Storage Rack System Heavy Duty Pallet Warehouse Solution

Commercial Industrial Storage Rack System Heavy Duty Pallet Warehouse Solution

View Specifications
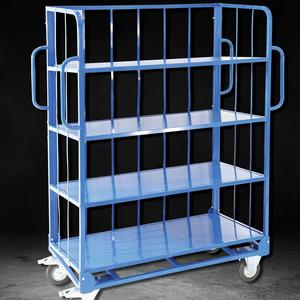
4 Layer Customizable Heavy Duty Metal Shelf Trolley Warehouse Order Picking Storage Cart

4 Layer Customizable Heavy Duty Metal Shelf Trolley Warehouse Order Picking Storage Cart

View Specifications
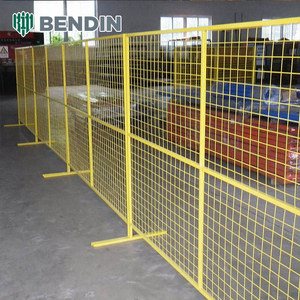
Custom Industrial Workshop Isolation Fence Perforated Metal Safety Barrier

Custom Industrial Workshop Isolation Fence Perforated Metal Safety Barrier

View Specifications
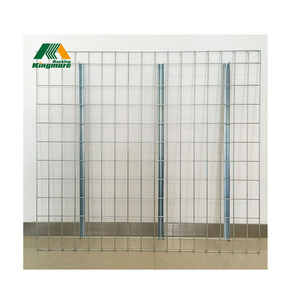
Galvanized/Powder Coated Wire Mesh Decking 1000kg Industrial Selective Pallet Racking

Galvanized/Powder Coated Wire Mesh Decking 1000kg Industrial Selective Pallet Racking

View Specifications
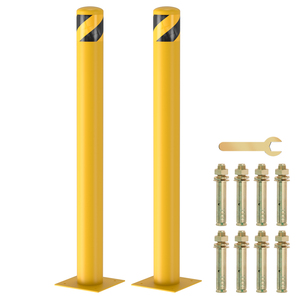
High Quality 42 Inch Heavy Duty Safety Yellow Safety Bollard Traffic Barriers

High Quality 42 Inch Heavy Duty Safety Yellow Safety Bollard Traffic Barriers

View Specifications
Heavy Duty Adjustable Metal Shelves Racking System Stacking Storage Pallet Racking

Heavy Duty Adjustable Metal Shelves Racking System Stacking Storage Pallet Racking

View Specifications
Warehouse Free Standing Modular Mezzanine Floor Kits With Stairway and Elevator

Warehouse Free Standing Modular Mezzanine Floor Kits With Stairway and Elevator

View Specifications
Customized Steel Mezzanine Floor with Safety Railing & Modular Platform Racks

Customized Steel Mezzanine Floor with Safety Railing & Modular Platform Racks

View Specifications
CE / EN1090
Certified Structural Compliance
3,000 KG
Max Stacked Load Rating per Unit
5-High
Safe Vertical Stacking Capability
25+ Years
Industrial Service Lifecycle Design

Engineering Excellence in CE Certified Post Pallet Racks Manufacturing

In modern high-throughput logistics, chemical processing, automotive assembly, and cold-chain infrastructure, dynamic spatial management is a primary operational determinant. CE Certified Post Pallet Racks (frequently designated across European supply chains as Manuracks, stacking frames, or post stacking pallets) represent a critical structural bridge between rigid, permanent selective pallet racking and volatile, floor-stacked bulk storage.

Unlike conventional static racking systems, post pallet systems offer modular vertical stackability without requiring permanent floor anchor bolt penetration. This provides facility managers with unprecedented flexibility to scale storage capacity seasonally, reconfigure floor pathways dynamically, or compress unused storage units into condensed nests during off-peak operational cycles.

Crucial Architectural Advantages of CE-Marked Post Pallets

The structural performance of post pallet systems hinges on precise metallurgical selection, certified automated welding, and finite element analysis (FEA) testing under dynamic load conditions. Key engineering advantages include:

  • Zero Permanent Footprint: Allows instant warehouse layout reconfiguration without specialized tools, drilling, or structural building alterations.
  • 3D Cube Utilization: Capitalizes on underutilized vertical space up to 5 tiers high, multiplying usable cubic storage density by up to 400%.
  • Damaged Goods Prevention: Load-bearing tubular corner posts bear 100% of upper level weights, eliminating crushed bottom-tier cartons or compromised shrink-wrapped goods.
  • Seamless Transportability: Built-in 4-way or 2-way heavy-duty forklift channels enable immediate transit of fully loaded post pallets directly onto flatbed trailers or containers.

Technical Specification Matrix: Structural Comparisons

Understanding the precise technical parameters separating standard commercial post racks from certified industrial-grade CE post pallets is essential for safety-conscious procurement teams.

Specification Parameter Standard Post Racks (Non-Certified) CE Certified Heavy-Duty Post Pallets Operational Impact & Value
Steel Grade Standard Commercial Grade Q195 / Scrap Steel Certified Q235B / Q355B Structural Carbon Steel Higher yield strength ($f_y \ge 355 \text{ MPa}$), superior impact resistance.
Compliance Certification Self-Declared / None CE Mark (EN 1090-1 / EN 15635 / ISO 3834-2) Legal compliance for EU/GCC safety audits; verified static/dynamic integrity.
Base Frame Construction Stamped Light Sheet Metal (1.8-2.0mm) Robotic-Welded Structural Channel / Heavy Tube (3.0-4.5mm) Prevents frame sagging under maximum point loads; extended service lifecycle.
Stacking Safety Ratio 2:1 Safety Factor 3:1 or 4:1 Verified Structural Safety Factor Resists accidental forklift impact, seismic vibrations, and off-center loading.
Corrosion Protection Finish Basic Single-Coat Solvent Paint Hot-Dip Galvanized (HDG ISO 1461) / Epoxy Powder Coating Resists rust down to -30°C cold storage environments and outdoors exposed to humidity.
Corner Post Interlock Loose Slip Fit Cup Precision-Machined Tapered Socket & Stacking Cup Eliminates vertical sway, tilt deviation, and risk of upper tier dislodgement.

Anatomy of a CE-Certified Post Pallet Rack

Heavy-Duty Stacking Cups

Engineered with deep tapered guide cones, these heavy-gauge forged steel cups allow crane or forklift operators to quickly seat upper corner posts into lower sockets even under poor line-of-sight conditions.

Reinforced Base Decking

Options include solid structural steel sheet, wire mesh decking for fire sprinkler penetration, or cross-tubular runners designed specifically to capture Euro and US Wooden/Plastic Pallets securely.

EN 1090 Certified Welds

Every load-bearing joint undergoes automated robotic MIG welding certified under ISO 3834-2 procedures, guaranteeing 100% weld penetration and preventing stress fatigue cracks under repeated loads.

Future Procurement Trends in Industrial Stacking Systems (2025–2030)

As global logistics networks transition toward automated material handling, carbon neutrality, and lean inventory strategies, procurement managers must evaluate post pallet rack suppliers against emerging technological standards:

1. AGV & AMR Guidance Compatibility

Modern post pallets are increasingly designed with precise laser-cut optical target zones and standardized under-chassis clearances to accommodate autonomous mobile robots (AMRs) and automated guided forklifts (AGVs).

2. Sustainable Coating Chemistry

Environmental regulations in Europe and North America favor zero-VOC electrostatic powder coating and eco-friendly lead-free hot-dip galvanizing, reducing life-cycle carbon footprints while maintaining 1000+ hour salt-spray test resistance.

3. Smart RFID & IoT Structural Tracking

Enterprise buyers are embedding passive RFID tags and smart load-cell sensors directly into post rack frames to track asset location across regional distribution centers and prevent structural overload scenarios.

Why Direct OEM Manufacturing Expertise Matters

Sourcing direct from an established, fully integrated racking manufacturer eliminates third-party markups while giving procurement leaders complete structural customization over length, width, height, load rating, and surface treatment.

With over two decades of structural engineering experience, our direct manufacturing infrastructure operates advanced automated roll-forming lines, 3D laser tube cutting machines, robotic welding cells, and an in-house surface preparation plant. From pre-production Finite Element Analysis (FEA) computer simulations to rigorous non-destructive weld testing, we guarantee that every batch meets stringent international safety mandates.

In-House Design CAD/FEA Structural Modeling
Full Traceability Raw Material Steel Mill Certificates
Custom Dimensions Tailored Post Lengths & Profiles
Global Shipping Knock-Down Export Packaging

Frequently Asked Questions (FAQ)

Answers to vital structural, safety, and logistical questions for B2B sourcing specialists.

1. What structural certifications must a legitimate CE Certified Post Pallet Rack carry?
A genuine CE certified post pallet system must comply with EN 1090-1 (Execution of steel structures and aluminium structures), EN 15635 (Steel static storage systems), and ISO 3834-2 for fusion welding. Manufacturers must provide factory production control certificates and Declaration of Performance (DoP) documentation for European market entry.
2. How high can CE Post Pallets be safely stacked when fully loaded?
Depending on base frame dimensions, corner post thickness, and total load weight, post pallets are typically rated for 3-high to 5-high vertical stacking. For instance, with a 1,500 kg payload per unit, a certified frame with heavy-wall 60mm structural tubing can safely support a total ground stack weight exceeding 6,000 kg.
3. Which finish is better for post pallets: Hot-Dip Galvanizing (HDG) or Powder Coating?
Hot-Dip Galvanizing (HDG) is recommended for extreme conditions, cold storage (-30°C), outdoor yard storage, and chemical exposure, as it coats both the interior and exterior of tubular posts with a protective zinc layer. Powder coating is cost-effective, ideal for indoor dry warehouses, and available in custom corporate colors.
4. How do post pallets maximize empty warehouse storage space during off-seasons?
Demountable post pallets allow removable corner posts to be unseated from corner sockets and laid flat within the base frame. This modular design enables 80% to 90% space recovery, allowing up to 20 empty bases to be nested vertically in a single floor position.
5. Can post pallet racks be customized for irregular or non-standard cargo?
Yes. As a direct OEM manufacturer, custom engineering can adjust base dimensions, post lengths, add side mesh retention walls, forklift guiding runners, removable dividers, or specialized cradle attachments for cylindrical items like textile rolls, steel coils, and tires.
6. What lead times and shipping container packing efficiencies can be expected?
Standard manufacturing lead times range from 2 to 4 weeks depending on batch volume. Knocked-down post pallets are tightly bundled and strapped onto steel skids, maximizing 40-foot High Cube (40HC) shipping container capacity and drastically reducing sea freight costs per unit.

Optimize Your Warehouse Density with Certified Post Racks

Consult directly with our structural engineering team today to receive CAD layouts, Finite Element Analysis load reports, and wholesale direct manufacturer pricing.

Contact Us