Procurement Engineering White Paper
Top 10 Cold Room Shelving Factories: Global Manufacturing Benchmarks
Cold chain logistics operations and industrial walk-in refrigeration facilities represent some of the harshest operating environments in the modern supply chain. The thermodynamic reality of sub-zero warehousing introduces complex physics: structural steel embrittlement, continuous moisture condensation cycles leading to rapid galvanic corrosion, and substantial refrigeration power loss caused by improperly configured, dense storage profiles that choke air circulation. Selecting a vendor from among the top 10 cold room shelving factories requires looking beyond mere catalog load capacity; it demands a granular evaluation of manufacturing tolerances, steel chemistry, protective metallurgy, and automated production consistency.
Information Gain Insight: Unlike ambient warehouse racking where room temperature allows standard carbon steels (such as generic Q235B or ASTM A36) to perform reliably, cold room environments operating from -20°C down to -40°C push structural steels past their Ductile-to-Brittle Transition Temperature (DBTT). When choosing a primary cold room shelving factory, procurement officers must demand Charpy V-notch impact toughness test certificates certifying at least 27 Joules at -20°C or -40°C (e.g., EN 10025 S355J2 or S355K2 grades). Failure to do so exposes facilities to sudden, catastrophic shear failure under minor forklift impacts.
Evaluation Criteria for Tier-1 Cold Room Shelving Manufacturers
Global logistics consultancies, 3PL giants, and cold chain operators assess manufacturing facilities against five primary engineering pillars:
- Continuous Roll-Forming Tolerances: Precision profile cold-forming lines capable of producing uprights and beams without residual stress concentrations or micro-fissures along bent radii.
- Surface Passivation & Galvanic Coatings: In-house Hot-Dip Galvanizing (HDG) per ISO 1461 (minimum 70–85 µm coating thickness) or pre-galvanized high-yield strip coils (Z275 to Z600 coatings) combined with food-grade antimicrobial thermoset epoxy-polyester coatings.
- Sub-Zero Connection Engineering: Hook-in connector brackets designed with 4-to-5-finger safety claws, cold-hardened safety pins, and thermal break baseplate isolators preventing thermal conductance into concrete foundation slabs.
- Hygiene & Cleanability (NSF/HACCP Compliance): Weld seams ground flush, closed box-beam profiles without hollow upward pockets that harbor moisture, bacteria, or listeria, and shelf decks with 50%+ open wire or slot perforation.
- BIM & Computational Fluid Dynamics (CFD) Layout Capacity: In-house engineering capabilities that calculate forced evaporator air distribution through pallet flues, preventing thermal dead spots and energy wastage.
| Evaluation Parameter |
Tier-1 Cold Room Factory (e.g., Signature Racking) |
Standard Commercial Rack Fabricator |
Generic Commodity Trader |
| Steel Grade & Impact Rating |
EN 10025 S355J2 / S355K2 (Charpy tested @ -20°C/-40°C) |
Standard Q235B / ASTM A36 (Untested DBTT) |
Recycled scrap steel (Unknown metallurgy) |
| Corrosion Protection |
HDG ISO 1461 (85 µm) or Z600 Galvanized + Antimicrobial |
Single-coat standard decorative powder coat |
Thin spray enamel (<30 µm), fast rusting |
| Airflow Perforation Ratio |
>50% Open area for laminar evaporator circulation |
Solid chipboard or unperforated sheet metal |
Wooden pallets or unvented decks |
| Design Code Compliance |
EN 15512, FEM 10.2.02, RMI, SEMA, local seismic |
Rudimentary static calculation only |
No certified structural verification |
| Thermal Bridging Isolation |
High-density polyamide / neoprene slab anchor thermal pads |
Direct metal-to-concrete anchor bolt fastening |
Direct unisolated surface mounting |
| Manufacturing Control |
100% In-House Roll Forming & Welding |
Partial outsourcing of punching and coating |
100% Brokered / Third-Party Sourced |
*Data collected through empirical cold chain auditing benchmarks across industrial freezers, chilled pharmaceutical stores, and meat packing walk-in cold rooms.
Energy-Density Optimization
Refrigeration energy comprises up to 65% of cold storage OPEX. Future procurement prioritizes ultra-dense mobile racking and deep-lane 4-way pallet shuttle systems, doubling cubic utilization while cutting conditioned air footprint by 40%.
Sub-Zero Autonomous AS/RS
Human ergonomics collapse rapidly at -25°C. Tier-1 cold facilities are transitioning to robotic picking grids and automated mini-load cranes. Shelving manufacturers must build to millimeter tolerances to allow robotic precision.
Eco-Friendly Galvanic Metallurgy
Stringent REACH and EPA environmental mandates are pushing factories away from toxic chromate conversion. Modern procurement requires eco-zinc-aluminum-magnesium (ZM) alloy coated steels delivering 3x higher corrosion protection than standard zinc.
CFD-Optimized Air Aerodynamics
Leading cold room shelf designs now utilize perforated wire decks and profiled channel flues mapped via Computational Fluid Dynamics (CFD). This eliminates stagnant thermal air pockets, ensuring perishable food remains safely below HACCP threshold lines.
Industrial Manufacturing Pedigree
Why Partner with Signature Racking Systems F.Z.C
Operating from our modern heavy industrial facility in Ajman Free Zone, United Arab Emirates, Signature Racking Systems F.Z.C has spent more than 20 years pioneering advanced storage rack engineering. Unlike brokers, trading agencies, or generic assemblers who outsource critical fabrication stages to third parties, Signature maintains complete, end-to-end sovereignty over every step of the manufacturing and quality assurance lifecycle.
Our dedicated engineering bureau, roll-forming workshops, automated CNC punching bays, certified structural welding stations, and electrostatic multi-stage coating plants guarantee microscopic tolerances, structural integrity, and documented quality that multinational cold chain clients demand.
Custom Roll-Forming Mill
Continuous automated profiling lines transforming prime structural steel coils into robust uprights and beams with zero structural residual micro-stress.
Automated CNC Punching
Multi-axis computerized punching ensuring a razor-precise 50mm and 75mm pitch repeatability across upright lengths up to 12 meters.
Certified Structural Welding
MIG/MAG welding executed by AWS and EN-certified master fabricators, guaranteeing connector lug joints hold rated shear loads under full dynamic shock loads.
Turnkey In-House Teams
From 3D CAD site surveys in Dubai, Abu Dhabi, or across the GCC, to knock-down export packaging and professional on-site anchoring and alignment verification.
Inside Our Ajman Manufacturing Facility
Take an inside look at our raw material verification, high-speed cutting, hydraulic pressing, continuous roll forming, and automated finishing lines.
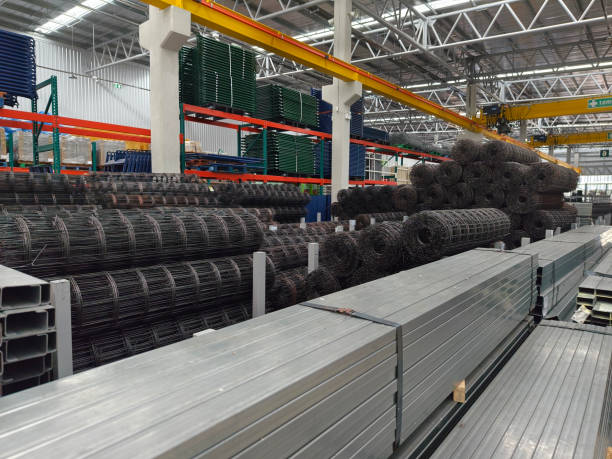
Raw Coil Intake
Verified High-Yield Steel
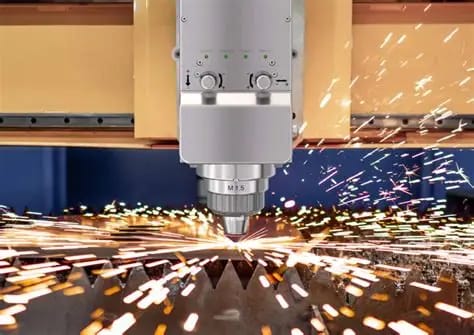
High-Speed Cutting
Accurate Beam Lengths
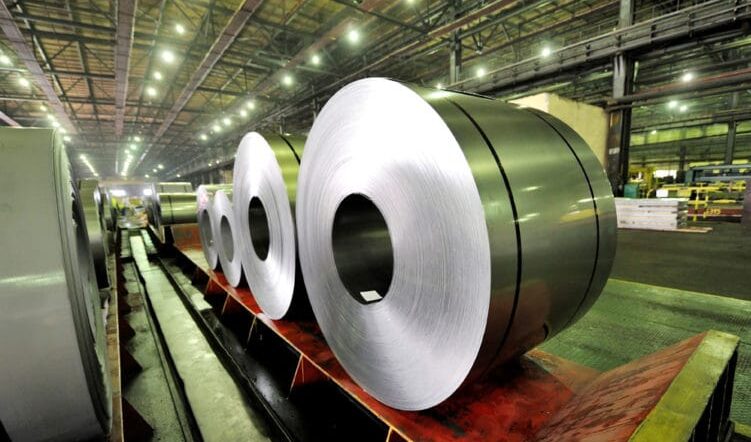
Roll Forming Bay
Custom Racking Profiles
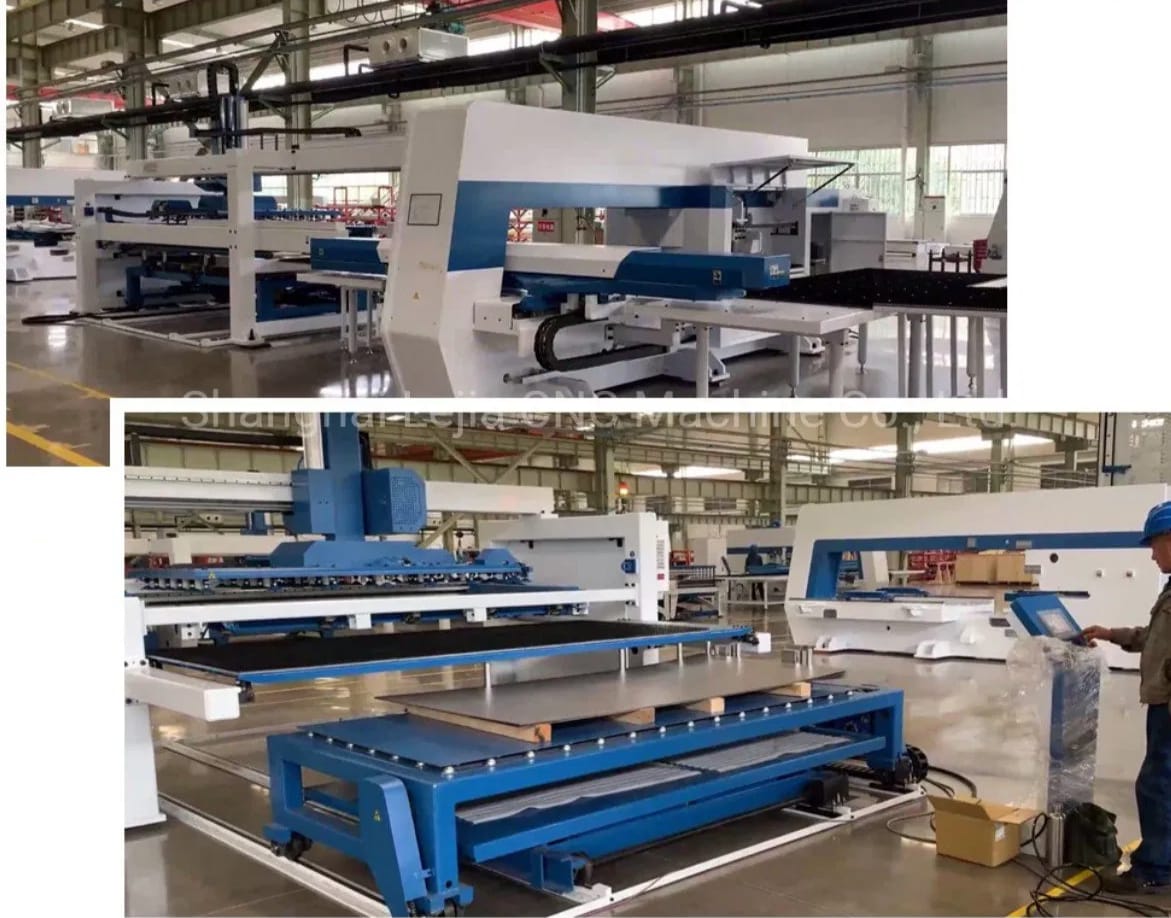
Automatic Punching
Micrometric Hole Pitch
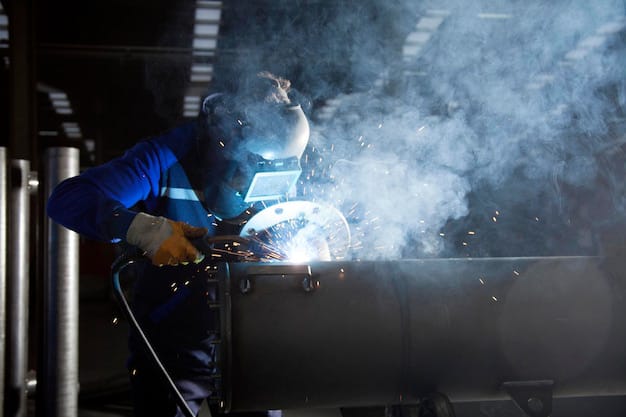
Precision Welding
High-Shear Joint Fusion
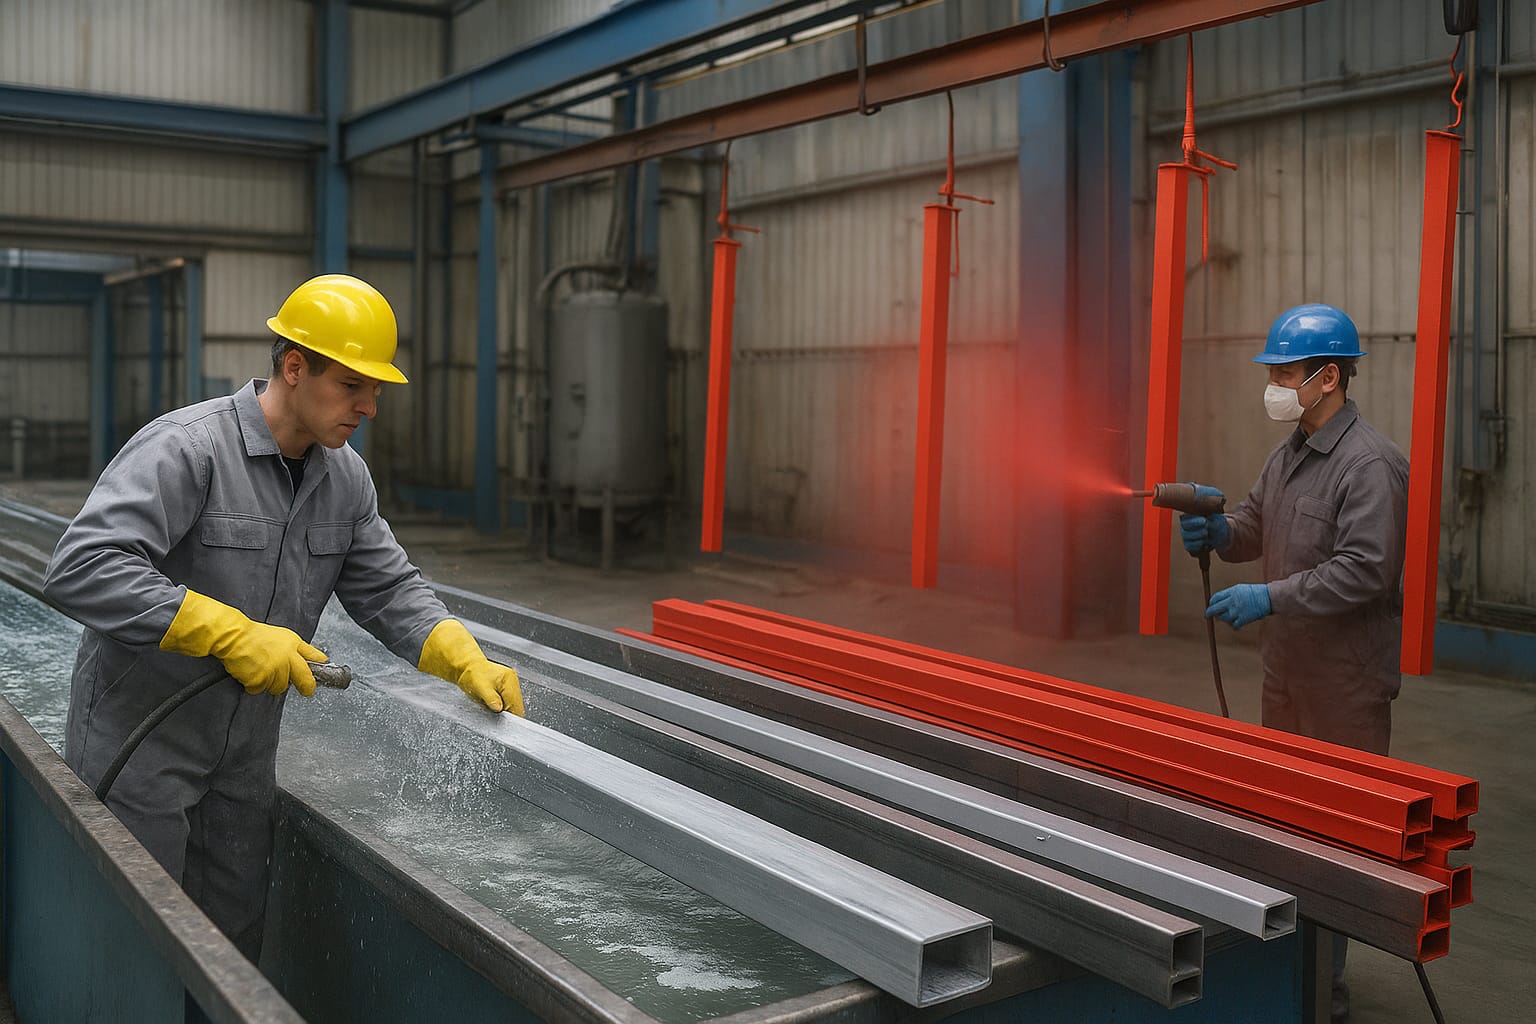
Washing & Powder Coating
Multi-Stage Pretreatment
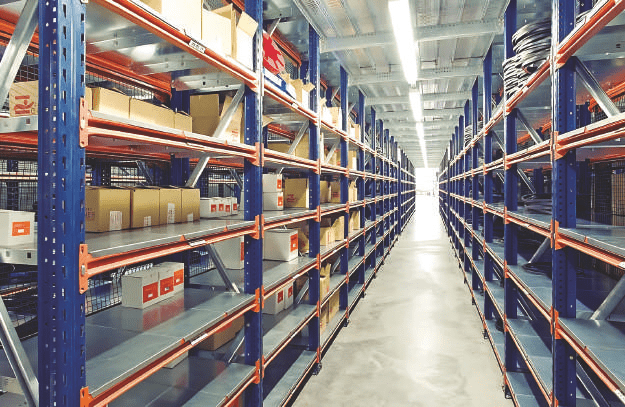
Installed Execution
High-Bay Project Handover
Global Distribution
Export-Packed Shipments